Normal industrial gear reducers emit a continuous, uniform, and low-amplitude meshing frequency. When mechanical deviations or surface fatigue develop, distinct acoustic patterns emerge. Maintenance personnel can diagnose internal root causes using a contact stethoscope or high-frequency vibration probe against the bearing seats.
| Acoustic Signature | Sound Characteristics | Primary Mechanical Root Cause | Immediate Action |
|---|---|---|---|
| Humming (Low Drone) | Continuous low-frequency drone; amplitude intensifies directly with torque load. | Tooth flank wear, micro-pitting, bearing raceway fatigue, or excessive gear backlash during direction reversal. | Sample oil for metal debris; inspect gear tooth flank profile and bearing clearances. |
| Clicking / Clunking | Sharp, rhythmic metallic impact (once per revolution) or random harsh clicks. | Fatigue tooth spalling, hard metallic contaminant in oil, broken tooth root, or loose shaft keyway/coupling. | Inspect oil sump with magnetic plug; boroscope tooth crowns immediately. Stop if cyclical impact occurs. |
| Shrieking / Whining | High-frequency whistling tone; pitch escalates with input shaft RPM. | Lubricant starvation, oil viscosity too low, bearing cage scuffing, or severe non-parallel shaft angular runout. | Emergency stop. Check oil level, verify ISO VG viscosity rating, and check high-speed bearing temperature. |
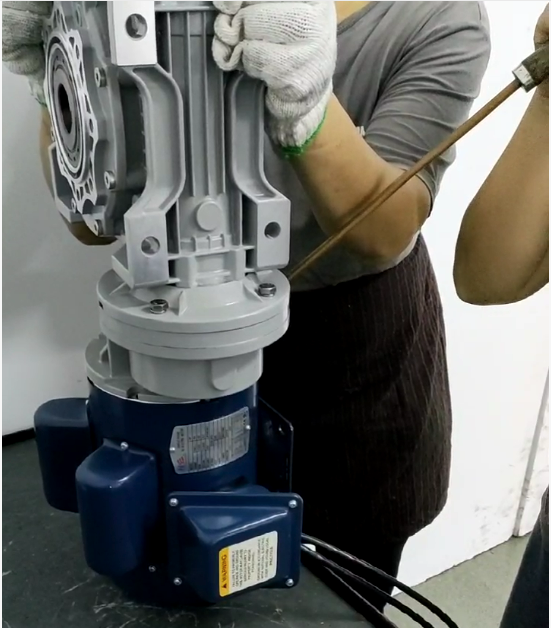
Figure 1: Locating internal acoustic emission sources on bearing caps and housing resonance points.
Controlling transmission noise requires looking beyond single components. Noise is excited by transmission errors under load and amplified by structural resonances across four lifecycle stages.
Under-sizing tooth contact width increases bending deflection under torque. Similarly, incorrect profile displacement coefficients generate meshing interference at root transition curves.
Carburizing and quenching (surface hardness > 58 HRC) cause micro-scale heat distortions. Pitch errors and lead runout concentrate loads onto tooth edges, raising noise by up to 12 dB.
Rigidly bolting an unaligned motor to a gearbox creates continuous cyclic bending moments on input bearings, triggering loud low-frequency structural vibration.
Improper lubricant viscosity causes film collapse under peak operating temperatures, leading to boundary contact and high-pitched friction squeal.
Noise control is engineered into every Wuma Drive transmission unit from the foundry to final dispatch. We address transmission noise at the source through automated high-precision machining and mandatory acoustic testing.
Every production batch of Wuma Drive reducers undergoes multi-speed operational testing inside our dedicated semi-anechoic sound chamber. High-sensitivity acoustic sensors capture decibel levels and spectral resonance across forward and reverse rotation cycles.
For automation lines, laboratory facilities, indoor packaging units, and theme park rides where low ambient noise is mandatory, choosing the right gearbox topology is more cost-effective than adding secondary acoustic insulation.
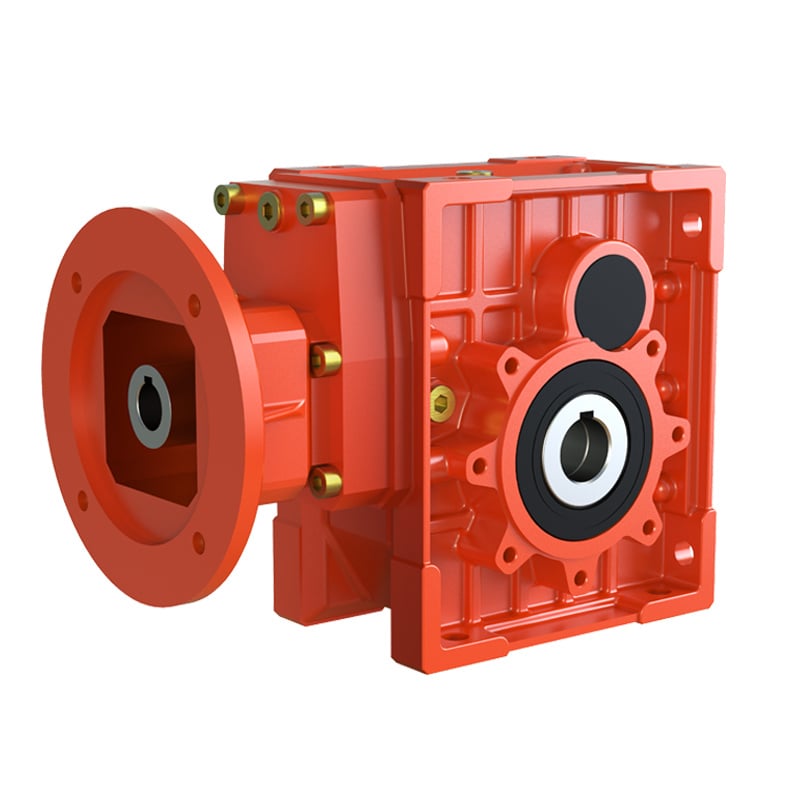
The ultimate low-noise alternative to worm drives. Features up to 90% transmission efficiency, smooth hypoid tooth rolling action, and lower heat generation. Ideal for servo automation, packaging, and compact machinery.
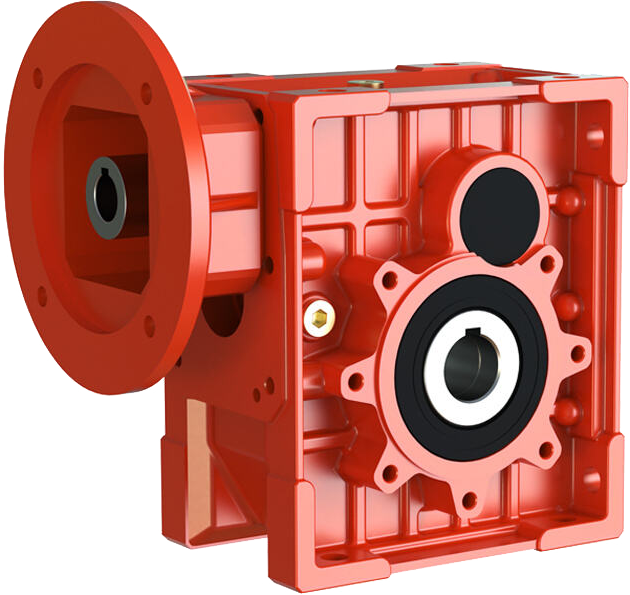
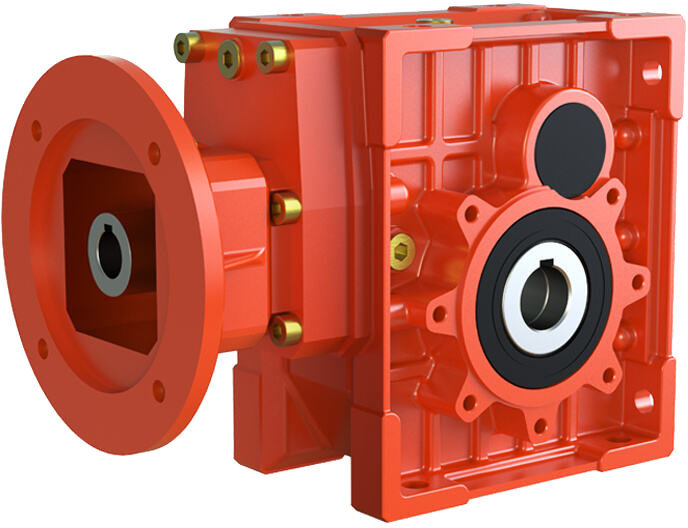
Noise rating: ≤ 65 dB(A) | Ratios: 7.5 – 300
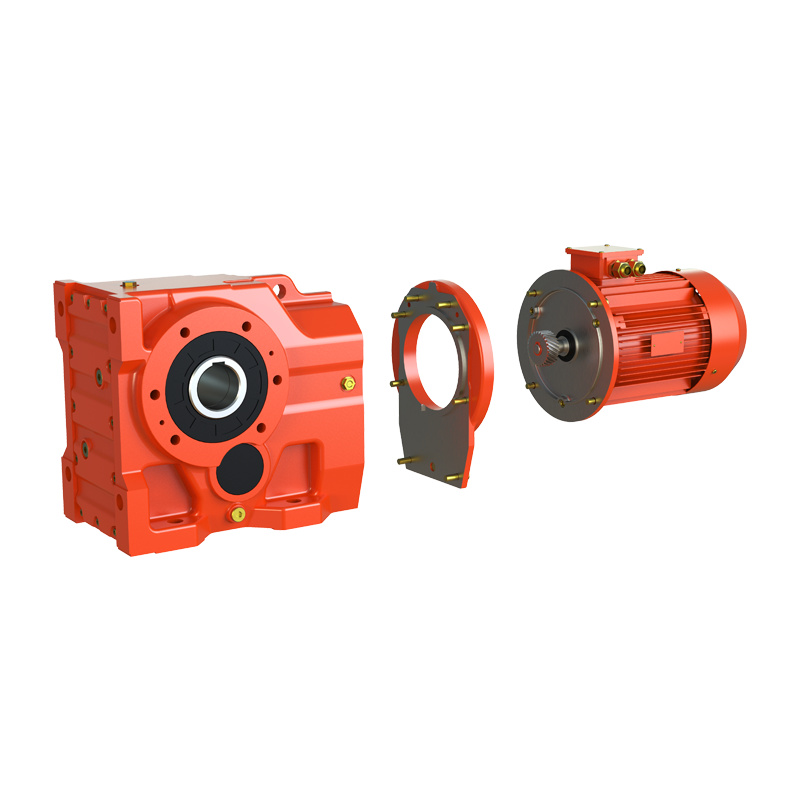
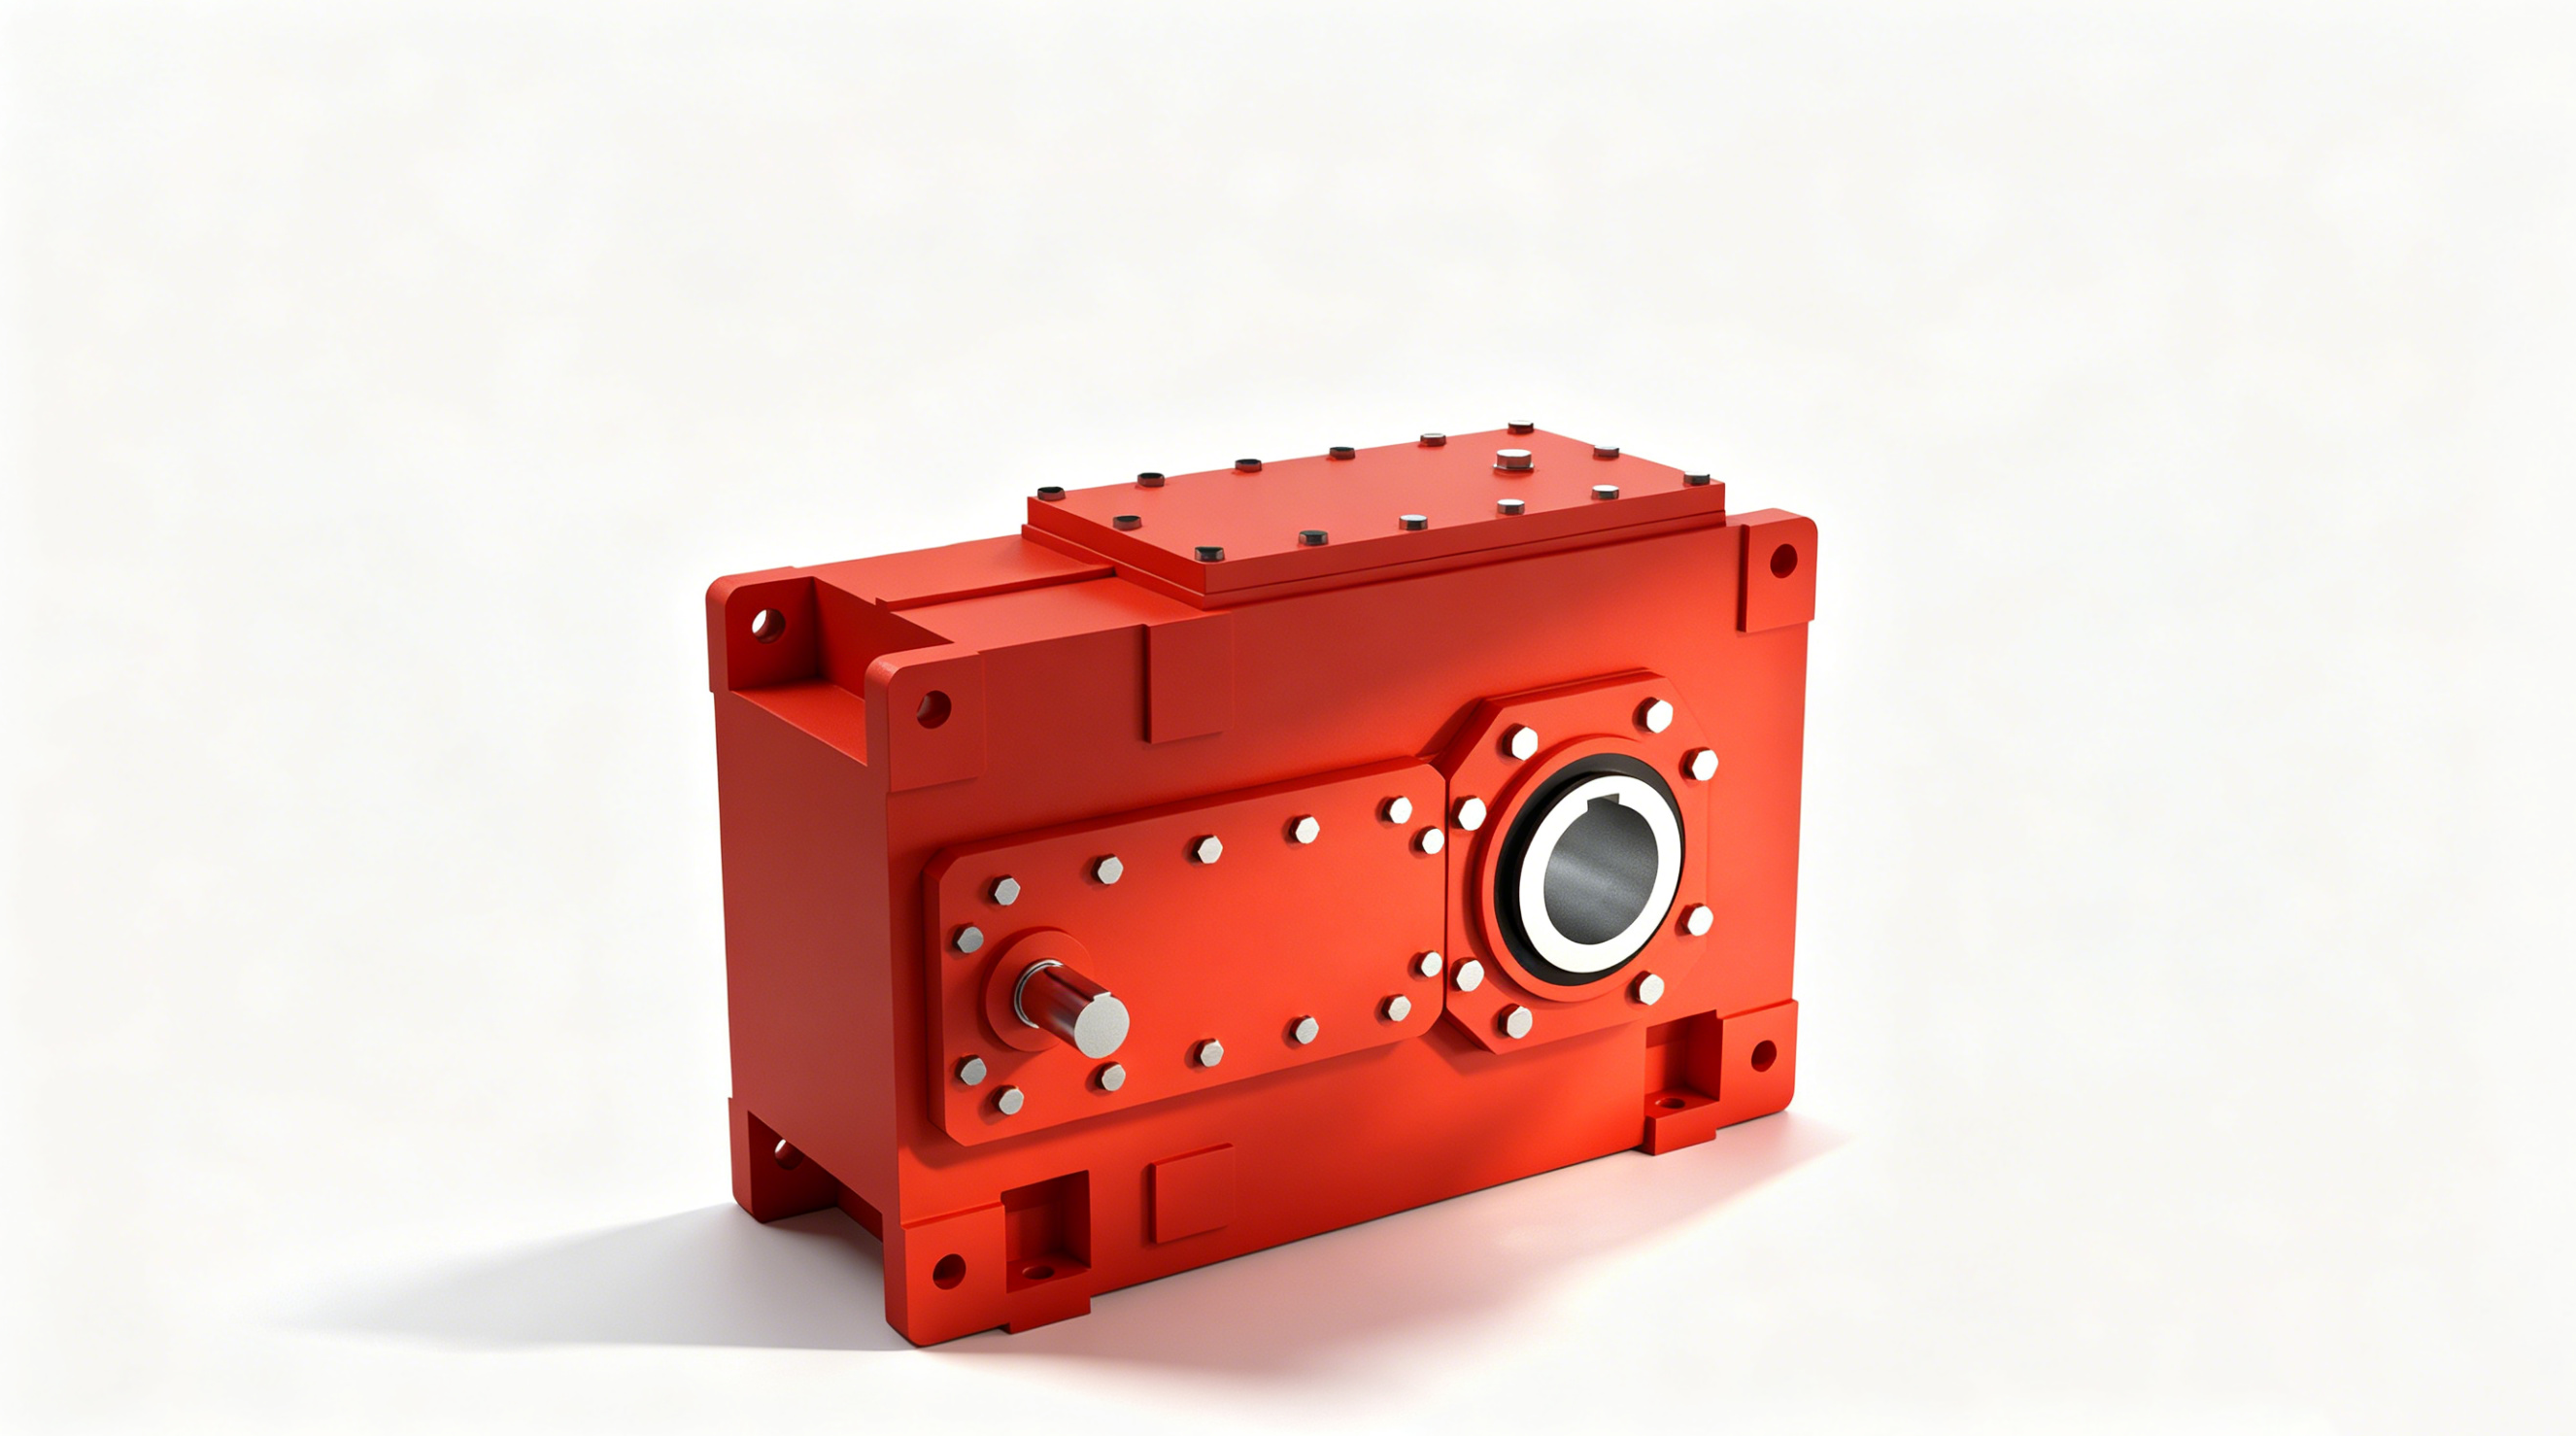
High-efficiency continuous drive. Progressive helical tooth engagement delivers over 96% efficiency with significantly reduced dynamic excitation compared to spur gears. Ideal for heavy-duty conveyors and mixers.
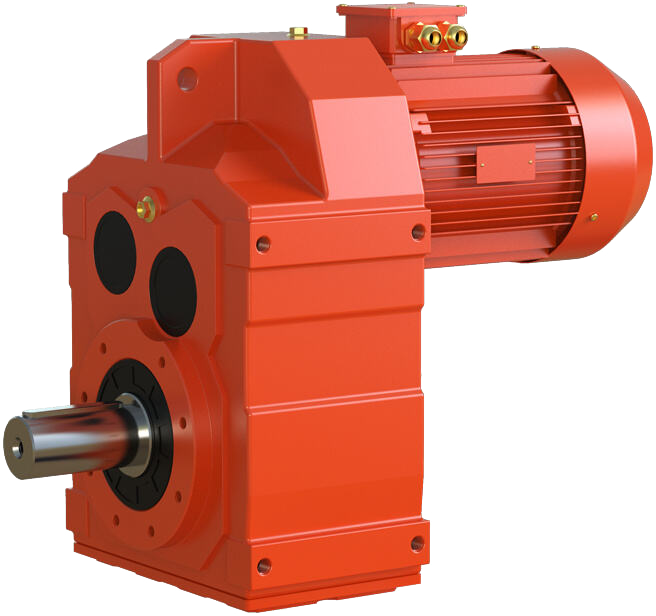
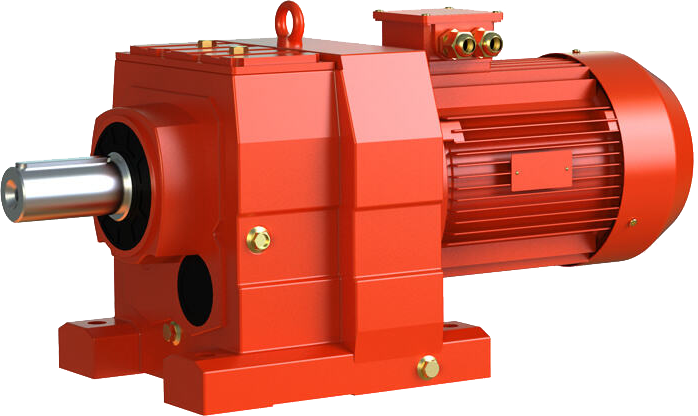
Continuous efficiency: > 96% | Precision ground teeth
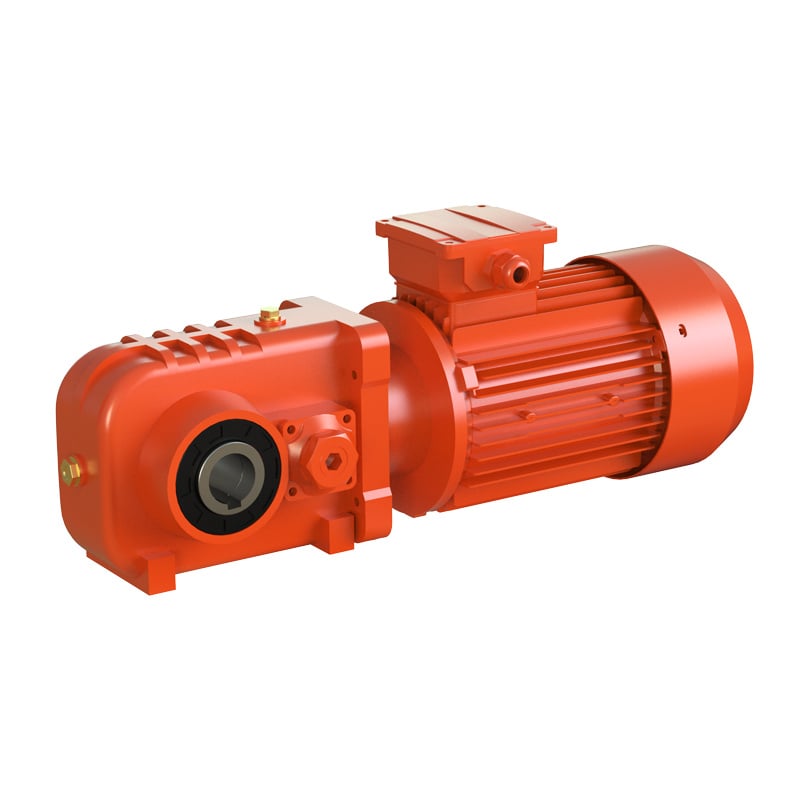
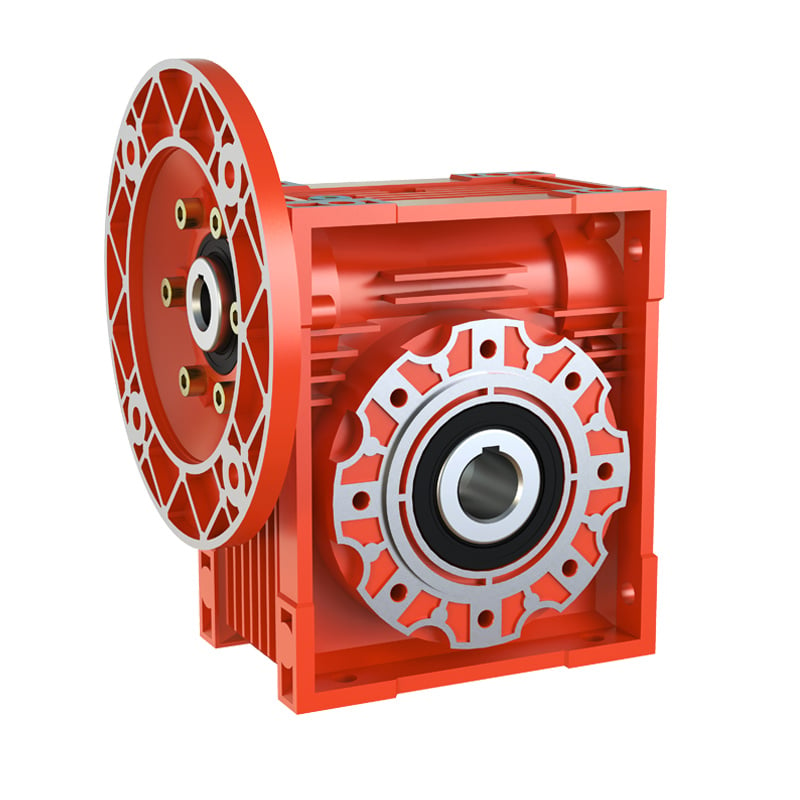
Quiet sliding meshing and self-locking safety. Compact die-cast aluminum casing paired with precision-finished bronze worm wheels for quiet, vibration-free operation in hoisting, lifting, and sorting.
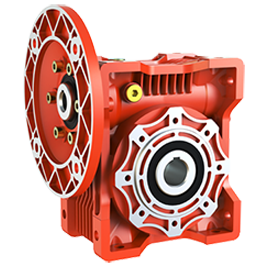
Smooth sliding contact | Drop-in universal mounting
Experiencing unresolved resonance in existing machinery? Share your motor RPM, operating torque, mounting layout, and ambient decibel target with Wuma Drive technical engineers for specialized acoustic optimization.
Custom gear tooth modifications & low-noise matching available.
Request Technical Review →Shrieking is typically caused by severe oil starvation, inadequate lubricant viscosity, or high-speed shaft bearing cage damage. Without an elastohydrodynamic oil film, direct metal-to-metal sliding friction generates loud whistle-like whine. Immediate shutdown is recommended to prevent tooth welding or bearing seizure.
Higher precision grades reduce tooth profile errors, base pitch deviations, and radial runout. Gears manufactured with precision ground and scraped tooth profiles produce 6 to 12 dB less operational noise compared to standard commercial gears under identical load conditions.
Worm gear pairs operate predominantly under sliding contact rather than pure rolling. When synthetic oil degrades or viscosity drops below ISO VG 320/460 standards, boundary friction spikes, causing thermal expansion, increased mesh friction, and elevated acoustic emission.
Wuma Drive enforces Grade 7 gear precision, precision tooth profile and root trimming, dynamic balancing of rotating assemblies, and mandatory 100% full-speed running tests inside a dedicated soundproof anechoic chamber before packaging.
Whether retrofitting noisy gearboxes or specifying quiet drivetrains for new automation lines, Wuma Drive engineers provide customized gear matching and acoustic compliance support.
 Hot News
2026-08-26
2026-08-18
2026-08-15
2026-08-11
2026-07-31
2026-07-29
Welcome to Wuma , a manufacturer committed to developing and manufacturing various types of gear reducers and gearmotors for the field of gear transmission.
No. 10, Xiangcun Industrial Zone, Dongyuan Town, Qingtian County, Lishui City, Zhejiang, China
Copyright © Zhejiang Wuma Drive Co., Ltd All Rights Reserved Privacy Policy Blog
 EN